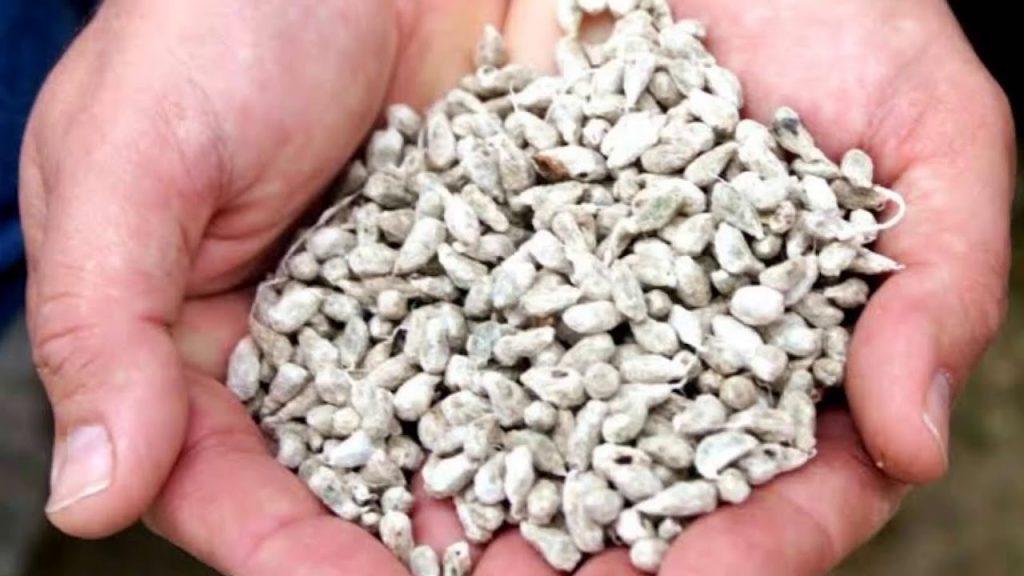
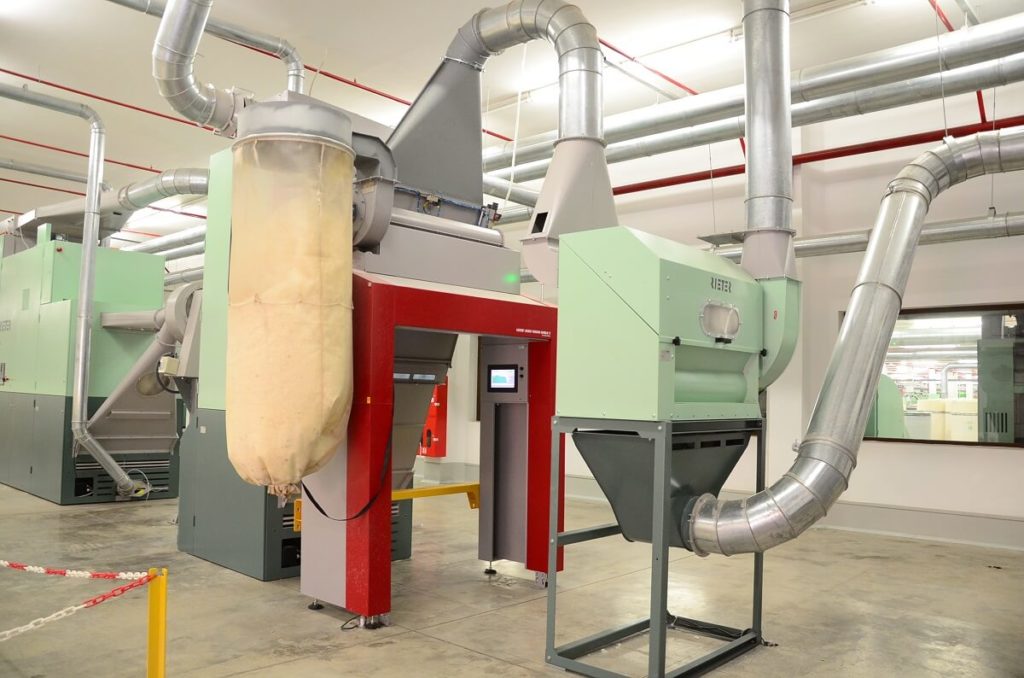
Sulton Tex Group also excels in seed processing, utilizing advanced technologies and industrial equipment to ensure the highest standards of efficiency and product quality. Our specialized facilities are equipped with automated production lines that enable a full cycle of cotton seed processing in accordance with international industrial standards. Sulton Tex Group facilities produce more than 30,000 tons of processed seeds annually
The processing cycle begins with the pre-cleaning stage, where raw materials undergo initial purification. At this stage, drum and vibrating cleaners, aspiration systems, and magnetic separators are used to remove mechanical impurities, dust, metal particles, and plant residues. This preparation ensures the stability of the technological process and protects equipment from excessive wear during subsequent processing stages.
The seeds then pass through the delinting stage, which removes short cotton fibers remaining on the surface of the seeds after the ginning process. High-performance delinting machines equipped with saw cylinders are used to carefully separate residual linter fibers. The extracted linters can be further utilized in other industrial sectors, including the production of cellulose-based materials and technical textiles.
Following this stage, the raw material undergoes calibration and sorting. Gravity separators, pneumatic sorting units, and modern quality control systems are used to classify seeds according to size, density, and physical characteristics. These technologies ensure uniformity of the processed material and improve the efficiency of further processing operations.
An important part of the process is thermal and mechanical treatment, which includes conditioning, drying, and stabilization of the seeds. Specialized drying equipment and temperature control systems maintain optimal moisture levels, helping preserve seed quality and ensuring stability during storage and transportation.
All stages of processing are integrated into a centralized automated production management system, which continuously monitors key technological parameters, optimizes operational efficiency, and ensures consistent product quality.